Complete thread code
Keep the final digit: codes such as 5V1 and 5V2 have different pitches.
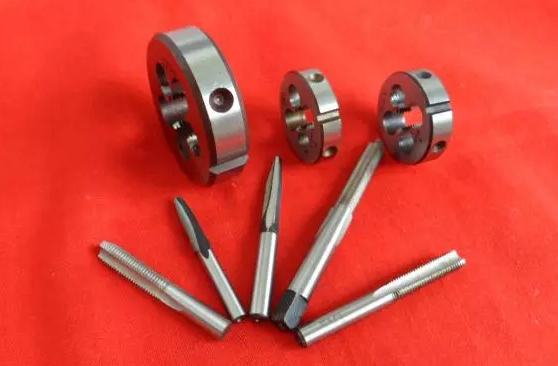
Catalog reference image. Final configuration is confirmed in the quotation.
19 VALVE THREAD CODES
Special tyre-valve thread taps with 19 catalog codes from 5V1 to 20V1. Compare the printed nominal diameter and pitch, then confirm the component thread and tap connection.
This series covers the special tyre-valve thread taps listed in the company catalog, from 5V1 to 20V1. Select the complete code and compare nominal diameter d and pitch P; matching the diameter alone is not enough. Use the component drawing and existing tool dimensions to confirm the thread profile, tolerance and machine connection.
Keep the final digit: codes such as 5V1 and 5V2 have different pitches.
Compare both d and P in the 19-row table before choosing a catalog reference.
Confirm the shank, square, thread depth, tolerance and gauge against the required drawing.
The tyre-valve tap table in the supplied FuRui catalog lists 5V1 and 5V2 at the same nominal diameter d = 5.2 mm. Their pitches differ: 0.705 mm for 5V1 and 1.058 mm for 5V2. A diameter measurement alone will not identify the correct replacement.
The same issue appears at 17V2 and 17V3: both list d = 17.5 mm, but P changes from 1.058 to 1.588 mm. Keep the complete catalog code, including its final digit, with the component drawing and mating-thread requirement.
Ask about 5V1 or ask about 5V2. The specifications table gives all 19 printed codes and their nominal d/P values.
These are catalog references for special tyre-valve thread taps. The listed nominal diameter and pitch do not specify a complete valve, establish sealing performance or replace the required thread tolerance and gauge.
For a production or replacement inquiry, identify the internal feature to be machined and provide the component drawing, material, full-thread depth and machine connection. Add the existing tap code, shank/square measurements and the required inspection points. If the request concerns an external thread or a combined cutter instead, state that separately and include its tool drawing.
The source table supports the code, nominal diameter and pitch shown here. Tool material, coating, tolerance, stock and production lead time remain quotation-specific. Round threading dies address external threads and are a separate selection.
Download the two-page threading selection reference with all 19 valve-thread codes (PDF, 9 KB). It includes the nominal diameter and pitch table, not a complete manufacturing drawing.
Nominal d and pitch P values in millimeters, transcribed from the supplied company catalog table headed Special Tap for valve of tyre (printed page 14). Codes are retained as printed. These are catalog references, not a stock list or a complete thread-standard specification. Confirm profile, tolerance, hand, shank/square, required thread depth and the final drawing before ordering. Merged length fields are not reproduced here.
Select an underlined catalog reference to include that row in your inquiry.
| Catalog thread code | Nominal diameter d (mm) | Pitch P (mm) |
|---|---|---|
| 5V1 | 5.2 | 0.705 |
| 5V2 | 5.2 | 1.058 |
| 6V1 | 6.0 | 0.800 |
| 8V1 | 7.7 | 0.794 |
| 8V2 | 7.9 | 1.058 |
| 9V1 | 9.4 | 0.794 |
| 10V1 | 9.6 | 1.000 |
| 10V2 | 10.3 | 0.907 |
| 11V1 | 11.1 | 1.270 |
| 12V1 | 12.2 | 0.907 |
| 13V1 | 12.6 | 1.27 |
| 13V2 | 12.7 | 0.794 |
| 15V1 | 15.0 | 1.000 |
| 16V1 | 15.8 | 0.941 |
| 17V1 | 17.0 | 1.000 |
| 17V2 | 17.5 | 1.058 |
| 17V3 | 17.5 | 1.588 |
| 19V1 | 19.0 | 1.588 |
| 20V1 | 20.5 | 1.000 |
No matching model in this table. Try a shorter code, or send your required size or drawing.
Ranges and slash-separated values describe catalog families, not every possible combination. Confirm the complete model and drawing before ordering.
Typical selection contexts for this series, not customer project claims. Confirm machine compatibility and cutting conditions for your setup.
Machining a threading feature defined by the specific valve-core drawing.
Combining a component profile requirement with a confirmed machine connection.
Matching a worn special tool from its drawing or physical sample.
Specify the dimensions, tolerances and records your order requires. Acceptance criteria must be agreed for the selected model.
Check the drawing reference faces and units. A catalog size alone does not define a tolerance or an inspection method.
List any required dimensional report, material document or model identification photograph in your inquiry. Confirm availability and scope in the quotation.
For a drawing-based part, include the drawing revision and identify the critical dimensions. Website photographs are not inspection reports.
Agree the packing method and photo requirements when confirming your order.
No verified shipment photographs for this series are currently published. Include selected-model, protective-packing and outer-label photos in your order requirements.
Discuss packing requirementsUse this checklist to agree what should be documented for your selected model.
Stock, dispatch date and shipping method are confirmed with the quotation. Website images are not live inventory evidence.
Keep a copy of the current series information for comparison. Confirm the final model and drawing before placing an order.
View specificationsPrepare the thread designation, workpiece drawing and tool connection.
Read the guideBrowse the existing tooling guides and compare product families before selecting a model.
Browse technical resourcesCompare alternative interfaces and complementary tooling. A related series is not automatically interchangeable.

55 DEGREE PIPE
CARBIDE COUNTERBORE SERIES
COMBINATION SERIES
No. The supplied catalog lists 19 distinct codes. For example, 5V1 and 5V2 both have nominal d = 5.2 mm but pitches of 0.705 and 1.058 mm respectively. Identify the complete code and confirm the component drawing, profile and tolerance.
The part is useful context, but tool connection, machine operation and a dimensional drawing are also needed.
No. The 19-row table lists special tyre-valve thread taps. External-thread dies and combined cutters require their own tool specification; do not use this table as their manufacturing drawing.
No product certification is established by this catalog entry. Tool inspection requirements must be specified separately.