Rigid holder format
The catalog describes a single rigid holder, not a telescopic compensation system.

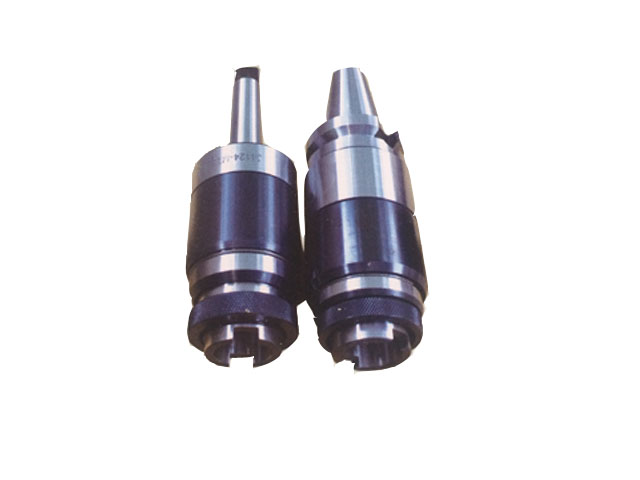
Catalog reference image. Final configuration is confirmed in the quotation.
MT-M
Rigid Morse taper tap holders: MT2-M for M3–M12, MT3-M for M6–M20 and MT4-M for M6–M24 catalog tap ranges. Check tap dimensions and the machine connection.
The MT-M series consists of single rigid tap holders with MT2, MT3 or MT4 Morse taper connections. Each catalog model has its own tap-size range. Select the machine-side taper and the tap's physical connection together, and confirm that the machine's tapping method is suitable for a rigid holder before defining the order.
The catalog describes a single rigid holder, not a telescopic compensation system.
MT2-M, MT3-M and MT4-M have different listed tapping ranges.
Provide the tapping method and tap geometry so the complete arrangement can be assessed.
M16 is outside the MT2-M catalog range of M3–M12. MT3-M lists M6–M20, but it also has an MT3 machine connection: its larger tapping range does not make it a replacement for an MT2 holder. Confirm the machine connection first, then check the tap shank, driving square and tapping cycle.
For a machine with a confirmed MT3 connection, start with the MT3-M catalog row and add the full M16 thread designation, tap shank and square dimensions, workpiece material, hole type and quantity. The listed range does not guarantee suitability for every material or tapping cycle. If you need to compare holder arrangements, read what to confirm before ordering a tap holder.
Dimensions are in millimeters unless otherwise stated. Confirm the final drawing before ordering.
Select an underlined catalog reference to include that row in your inquiry.
| Model | Morse taper | Tapping range |
|---|---|---|
| MT2-M | MT2 | M3-M12 |
| MT3-M | MT3 | M6-M20 |
| MT4-M | MT4 | M6-M24 |
No matching model in this table. Try a shorter code, or send your required size or drawing.
Ranges and slash-separated values describe catalog families, not every possible combination. Confirm the complete model and drawing before ordering.
Typical selection contexts for this series, not customer project claims. Confirm machine compatibility and cutting conditions for your setup.
Selecting a tap holder for a confirmed machine connection and cycle.
Keeping one holder setup for a defined tap and thread requirement.
Matching an existing rigid holder by taper, code and tap connection.
Specify the dimensions, tolerances and records your order requires. Acceptance criteria must be agreed for the selected model.
Check the drawing reference faces and units. A catalog size alone does not define a tolerance or an inspection method.
List any required dimensional report, material document or model identification photograph in your inquiry. Confirm availability and scope in the quotation.
For a drawing-based part, include the drawing revision and identify the critical dimensions. Website photographs are not inspection reports.
Agree the packing method and photo requirements when confirming your order.
No verified shipment photographs for this series are currently published. Include selected-model, protective-packing and outer-label photos in your order requirements.
Discuss packing requirementsUse this checklist to agree what should be documented for your selected model.
Stock, dispatch date and shipping method are confirmed with the quotation. Website images are not live inventory evidence.
Keep a copy of the current series information for comparison. Confirm the final model and drawing before placing an order.
View specificationsIdentify the machine connection, tap shank and driving square.
Read the guideBrowse the existing tooling guides and compare product families before selecting a model.
Browse technical resourcesCompare alternative interfaces and complementary tooling. A related series is not automatically interchangeable.
BT-GT

STANDARD TAP SERIES
G SERIES
The source calls it a rigid holder and provides no compensation specification.
No. MT2-M is listed for M3–M12; use the range belonging to the chosen model.
No. The machine cycle and the complete toolholding arrangement must be suitable and confirmed.
Provide the tap designation, shank and driving-end dimensions, required reach and machine tapping method.